How Disconnected Systems Disrupt Manufacturing Supply Chains
Disconnected systems disrupt manufacturing supply chains when purchasing, inventory, production, warehousing, and order management operate with separate or outdated information. This can lead to material shortages, inaccurate stock records, production delays, and difficulties fulfilling customer orders. Supply chain integration helps manufacturers connect these operations and make decisions using more consistent information.
As manufacturing businesses grow, their operations become increasingly dependent on one another. Purchasing needs to understand material requirements, production needs accurate inventory information, warehouses need visibility into completed goods, and sales teams need reliable order updates.
However, when every department maintains its own applications, spreadsheets, or manual records, keeping these activities coordinated becomes difficult.
The problem is not necessarily the number of software tools a manufacturer uses. Multiple applications can work effectively when they exchange information reliably. The real challenge begins when departments cannot access the updates they need without repeated communication, manual data entry, or record reconciliation.
Understanding these gaps is the first step toward improving manufacturing supply chain integration.
What Are Disconnected Systems in Manufacturing Supply Chains?
Disconnected systems are separate software applications, spreadsheets, databases, or manual processes that manage different business activities without reliably sharing information.
A manufacturer might use one application for purchasing, another for inventory, spreadsheets for production planning, and separate software for customer orders. Each department may complete its individual tasks, but the information maintained by one department may not reflect the latest activities of another.
Consider a simple example.
A purchasing department receives raw materials, but the inventory spreadsheet is not updated immediately. Production planning continues using the previous stock figures. Meanwhile, the sales department confirms an order based on an expected production completion date.
Although every department is working, they are not necessarily working with the same information.
This can create:
Duplicate data entry across applications.
Different stock figures between departments.
Delays in communicating purchasing and production updates.
Difficulty tracking material requirements.
Repeated manual verification of customer orders.
Limited visibility into the overall manufacturing supply chain.
It is important to distinguish between multiple applications and disconnected systems. A business does not necessarily need to replace every existing application to achieve better integration. Suitable integrations can connect different tools, while an integrated ERP environment can bring major business functions into a more unified operational structure.
The right approach depends on the manufacturer's existing systems, processes, and requirements.
Where Disconnected Systems Create Problems Across Manufacturing Operations
Supply chain activities are connected. A problem in one department can affect several other departments, even when their individual processes are working as expected.
Purchasing Decisions Without Accurate Inventory Information
Purchasing decisions depend on accurate information about available materials, existing requirements, pending orders, and expected consumption.
When purchasing and inventory records are maintained separately, procurement teams may not have a reliable picture of current stock.
For example, a purchasing employee may order additional raw materials because the available spreadsheet shows insufficient quantities. However, the warehouse may have already received a shipment that has not been recorded in the purchasing records.
The opposite can also happen. Purchasing may delay an order because the system shows sufficient stock, even though some materials have already been consumed or allocated to production.
These situations can result in unnecessary purchasing, excess inventory, material shortages, and delays in procurement.
A connected purchasing and inventory workflow helps departments work with more consistent information when evaluating material requirements and stock availability.
Inventory Records That Do Not Match Actual Stock
Inventory accuracy is essential for manufacturing because production schedules, purchasing decisions, and order fulfillment depend on knowing what materials and finished goods are actually available.
Stock changes continuously through receipts, issues, transfers, returns, adjustments, and production consumption.
When these activities are recorded in separate systems or updated manually, inventory records may not reflect the latest movements.
For manufacturers operating multiple warehouses, the challenge becomes even greater. A material might be available at one location but unavailable at the location where production requires it.
Common consequences include:
Employees spending time verifying physical stock.
Production planning based on incorrect quantities.
Unnecessary purchasing due to incomplete stock information.
Difficulty tracking warehouse transfers.
Delays in fulfilling orders because finished goods availability is unclear.
The objective of inventory management is not simply to maintain a list of products and quantities. Manufacturers need reliable information about where materials are stored, how they move, and how much remains available for operational requirements.
Production Planning Without Reliable Material Visibility
Production planning requires an understanding of customer requirements, material availability, production routes, work orders, and expected output.
When production planning operates independently from purchasing and inventory, managers may schedule work without knowing whether all required materials are available.
For example, a production order may be scheduled for Monday, but the required material is still pending from a supplier. If this information does not reach the production team, the schedule may need to be changed at the last moment.
Other problems can include unexpected material shortages, production interruptions, inaccurate completion estimates, and difficulty comparing planned material consumption with actual usage.
Manufacturers also need to understand what happens after production begins. Knowing the planned material requirement is useful, but management also needs visibility into what production actually consumes.
Without this information, identifying material variances and investigating production inefficiencies becomes more difficult.
Delays Between Production Completion and Customer Dispatch
Manufacturing does not end when a production order is completed.
Finished goods may still need to be recorded, transferred to a warehouse, inspected, allocated to customer orders, picked, packed, and prepared for dispatch.
If production, warehouse, sales, and dispatch teams maintain separate records, information can become inconsistent during these stages.
Production might mark an order as completed while the warehouse has not yet confirmed the finished quantity. Sales may assume the goods are ready for delivery even though warehouse verification or other activities are still pending.
This creates a gap between production completion and actual customer dispatch.
The consequences may include incorrect order status, delayed dispatch preparation, confusion about finished goods quantities, and unreliable delivery commitments.
Manufacturers therefore need visibility beyond the production floor. They need to understand how completed goods move through warehousing and order fulfillment.
Warning Signs That Your Manufacturing Business Has Outgrown Disconnected Systems
Disconnected systems do not always cause an immediate operational failure. Their impact often becomes more noticeable as a business expands its products, departments, warehouses, and production volumes.
The following signs suggest that existing systems may no longer provide sufficient operational coordination.
Repeated manual data entry: Employees enter the same product, supplier, customer, or inventory information into multiple applications.
Frequent record reconciliation: Departments regularly contact one another to verify stock quantities, production progress, purchasing updates, or order status.
Conflicting departmental information: Management receives different figures for inventory, production output, pending orders, or material consumption.
Increasing spreadsheet dependency: Employees maintain separate spreadsheets because existing applications do not provide the information required for their daily work.
Difficulty identifying operational delays: Managers struggle to determine whether an order is delayed because of purchasing, material availability, production, warehousing, or dispatch.
Growing complexity across locations: Adding warehouses, production facilities, product categories, or sales channels makes information management increasingly difficult.
One warning sign alone does not necessarily mean a manufacturer needs to replace its software infrastructure. However, repeated problems across several departments indicate that information flow and system integration deserve attention.
What an Integrated Manufacturing Workflow Looks Like in Practice
Understanding the difference between disconnected and integrated operations becomes easier when looking at an actual manufacturing workflow.
Consider a manufacturer producing industrial machinery. The business needs to define the product structure, identify required materials, plan production, record consumption, and review manufacturing performance.
These activities should not be treated as unrelated tasks.
Step 1: Define the Product Structure Through a Bill of Materials
A Bill of Materials (BOM) defines the materials, components, quantities, and sub-assemblies required to manufacture a product.
For example, a finished machine may require a motor, housing, bearings, cables, fasteners, and several other components.
A multi-level BOM can also represent sub-assemblies that contain their own materials and components.
The BOM provides the material structure that purchasing, inventory, and production planning can use to understand what a product requires.
If the product structure is inaccurate or outdated, subsequent material planning can also become unreliable.
Step 2: Define How the Product Moves Through Production
After defining the product structure, the manufacturer needs to establish how the product moves through its production process.
This may involve manufacturing routing, work centers, machines, and the sequence of production activities.
For example, an industrial machine might pass through cutting, machining, assembly, and finishing stages.
The routing helps define the production path rather than treating manufacturing as a single activity.
Step 3: Create the Production Work Order
A production work order identifies what needs to be manufactured.
The production team can use the defined product structure and production requirements to manage the manufacturing activity.
Different manufacturing models may require different work-order approaches. Discrete manufacturing commonly deals with individual products or assemblies, while process manufacturing can involve batch-based or continuous production.
Multi-Techno's Production Management module includes both Discrete Work Order and Process Work Order functionality.
Step 4: Plan Materials Before Production
Before production begins, manufacturers need to understand whether the required materials are available or need to be arranged.
Multi-Techno's Production Management module includes:
Material Planning Sale Order Wise.
Material Planning Work Order Wise.
These features provide different planning approaches based on sales orders and production work orders.
The purpose of material planning is to help manufacturers identify requirements before they become unexpected production-floor shortages.
Step 5: Record Actual Production and Material Consumption
A production plan describes what the manufacturer expects to produce and consume. Actual manufacturing activity may differ from that plan.
For example, a production order may require 100 kg of a particular material, while the actual production process consumes 108 kg.
That difference needs investigation. It may relate to process loss, scrap, rework, measurement differences, or an incorrect material requirement.
Multi-Techno's Production Management workflow includes Work Progress and Material Consumption activities, helping manufacturers record production-related information.
Step 6: Review Planned and Actual Performance
Recording production information is useful, but management also needs reports that help evaluate what happened.
Multi-Techno's documented Production Management features include:
Actual vs. Plan Consumption Summary: For reviewing planned and actual material consumption.
Daily Actual vs. Plan Consumption Report: For examining consumption differences over daily production activity.
Work Order Status Report: For reviewing work-order status.
Down Time Report: For reviewing reported downtime.
Daily Production Route Wise: For reviewing production information by route.
These reports help move manufacturing management beyond simply knowing what was planned. They provide information that can support further investigation into material usage, production progress, and operational performance.
The important distinction is that a BOM defines what materials are expected, production records capture what happens, and reporting helps management evaluate the difference.
Want to see this workflow in practice? Book a Multi-Techno manufacturing ERP demo and explore how BOM, work orders, material planning, consumption, and production reports fit into the Production Management workflow.
Disconnected vs. Connected Manufacturing Operations
The difference between disconnected and connected operations is not simply the software being used. It is how effectively information moves between business functions.
Use this checklist to evaluate your current manufacturing setup.
Purchasing and inventory
Disconnected: Purchasing decisions depend on separately maintained stock records.
Connected: Relevant purchasing and inventory information can be shared through an integrated workflow.
Inventory and production
Disconnected: Production teams may need to confirm material availability manually.
Connected: Material requirements and inventory information can support production planning.
Production and material consumption
Disconnected: Planned quantities and actual consumption may be recorded separately.
Connected: Production-related material consumption can be recorded and reviewed against planned requirements.
Production and finished goods
Disconnected: Warehouse teams may receive delayed updates about completed production.
Connected: Production completion information can be coordinated with finished goods recording and warehouse processes.
Management reporting
Disconnected: Managers collect information from different applications and spreadsheets.
Connected: Relevant operational information can be reviewed through shared records and reporting workflows.
However, connected operations do not automatically guarantee accurate information. Data quality, process configuration, employee adoption, and the suitability of integrations remain important.
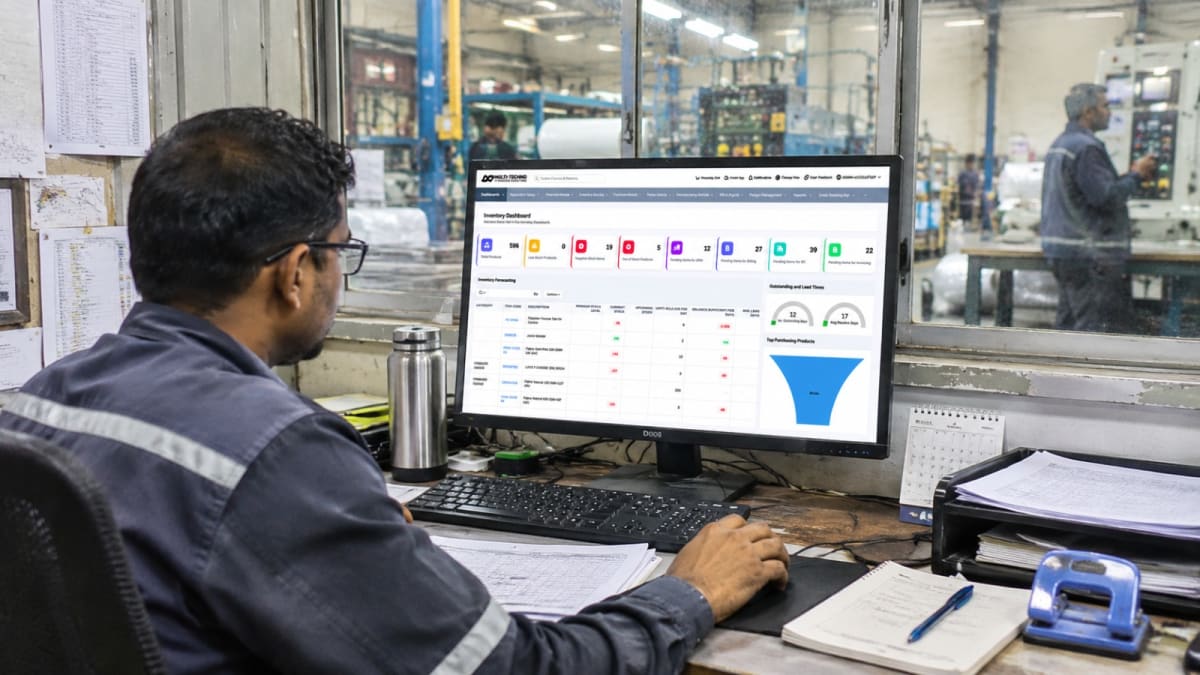
What Manufacturers Should Evaluate Before Integrating Their Supply Chain Systems
Manufacturers should understand their existing operational problems before selecting new software or connecting applications.
Map the Existing Information Flow
Identify how information moves between purchasing, inventory, production, warehousing, sales, and dispatch.
Determine where information is created, who updates it, which departments depend on it, and where manual communication is required.
This can reveal duplicate records, unnecessary steps, delayed updates, and missing information.
Identify Departmental Requirements
Each department needs access to information relevant to its responsibilities.
Purchasing may need material requirements and supplier information. Production needs work orders and material availability. Warehouse teams need stock movement and location records.
Defining these requirements helps establish what the integration should accomplish.
Evaluate Integration Compatibility
If a manufacturer intends to retain existing applications, it should evaluate whether those systems can exchange information reliably.
This may involve reviewing APIs, data formats, synchronization methods, integration costs, and technical limitations.
Not every application can be connected in the same way, so compatibility should be assessed before implementation.
Review Data Accuracy and Migration
Introducing a new system does not automatically correct inaccurate historical records.
Product details, supplier information, customer records, inventory quantities, and existing transactions should be reviewed before migration or integration.
Inconsistent source data can continue creating problems even after new software has been introduced.
Consider Customization and Future Growth
Manufacturers may have different production models, approval workflows, inventory structures, and reporting requirements.
A suitable solution should support the actual business process rather than forcing every manufacturer into an identical workflow.
Future requirements also matter. New warehouses, product lines, users, and production facilities should be considered when evaluating scalability.
How Integrated ERP Supports Better Manufacturing Supply Chain Coordination
An integrated ERP system can help manufacturers coordinate major business functions through shared operational information and connected workflows.
For example, purchasing, inventory, and production information can be managed through related modules instead of relying entirely on separate records.
This can support better coordination across several areas:
Purchasing and inventory: Material receipts and purchasing transactions can be reflected in inventory processes, helping departments maintain more consistent stock information.
Inventory and production: Material availability and production requirements can be considered together when planning manufacturing activities.
Production and finished goods: Completed production quantities can be recorded and coordinated with finished goods inventory processes.
Sales orders and fulfillment: Customer order requirements can be considered alongside stock availability and production requirements.
Warehouse and dispatch: Warehouse and dispatch teams can use relevant order and inventory information to coordinate finished goods movement.
For manufacturers with more complex operations, a manufacturing ERP may also need customization to accommodate specific production methods, approval processes, inventory structures, and reporting requirements.
The objective is not simply to put every department on the same software platform. It is to establish reliable processes through which the right information reaches the right people when they need it.
An ERP implementation should therefore be evaluated against actual business requirements, available features, integration capabilities, and the manufacturer's operational structure.
Final Thoughts
Disconnected systems can gradually disrupt manufacturing supply chains by creating information gaps between purchasing, inventory, production, warehousing, and customer dispatch.
These problems are not always caused by individual departments performing poorly. Often, employees are working with different records because their systems do not communicate effectively.
For growing manufacturers, the important step is to identify where these gaps exist and understand how they affect daily operations.
Adding more software may improve individual tasks, but sustainable improvement requires reliable information flow across the manufacturing business.
Whether through integrating existing applications or implementing an integrated ERP system, manufacturers should focus on connected processes, accurate records, coordinated decisions, and better operational visibility.
If your manufacturing business is evaluating ways to connect purchasing, inventory, production, and supply chain operations, book a Multi-Techno manufacturing ERP demo. Discuss your current workflow with the team, explore the relevant manufacturing capabilities, and evaluate how the solution fits your operational requirements.
Frequently Asked Questions
1. What are disconnected systems in manufacturing?
Disconnected systems are separate software applications, spreadsheets, or manual processes used by different departments without reliable information exchange. They can create inconsistent records and make it difficult to coordinate purchasing, inventory, production, and order fulfillment.
2. How do disconnected systems affect supply chain management?
They can cause inaccurate inventory records, delayed purchasing decisions, production interruptions, communication gaps, and difficulties tracking customer orders. These issues reduce operational visibility and make supply chain coordination more challenging.
3. What is supply chain integration in manufacturing?
supply chain integration in manufacturing involves connecting relevant business processes and systems so information can move between purchasing, inventory, production, warehousing, and order fulfillment. The objective is to improve coordination and support decisions based on consistent operational information.
4. How does ERP connect purchasing, inventory, and production?
An integrated ERP system can connect these functions through shared records and related business transactions. Purchasing updates can affect inventory information, while material availability and production requirements can be coordinated through connected processes.
5. When should a manufacturer integrate its supply chain systems?
A manufacturer should evaluate integration when departments frequently maintain duplicate records, employees rely heavily on manual updates, inventory information becomes inconsistent, or production and order fulfillment are regularly affected by communication gaps.
6. What should manufacturers consider when choosing supply chain software?
Manufacturers should evaluate operational requirements, integration capabilities, inventory visibility, production coordination, data migration, customization, implementation costs, reporting, and future scalability. The right solution should support actual business processes rather than simply offering a large number of features.